BIFA AutomationBIFA AutomationBuild Future
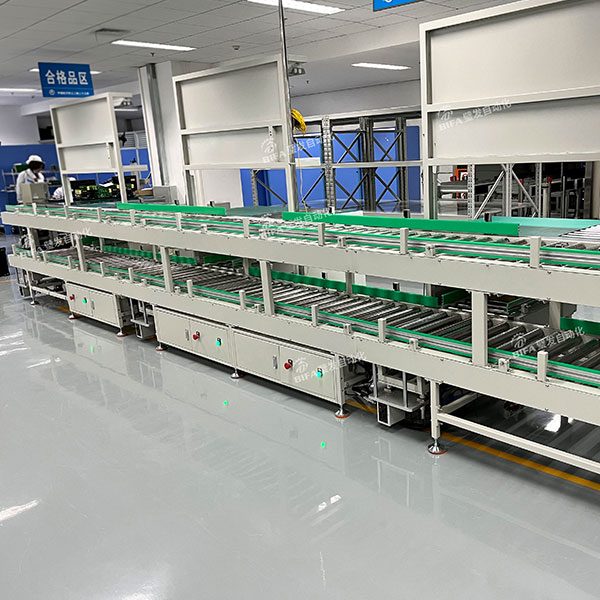
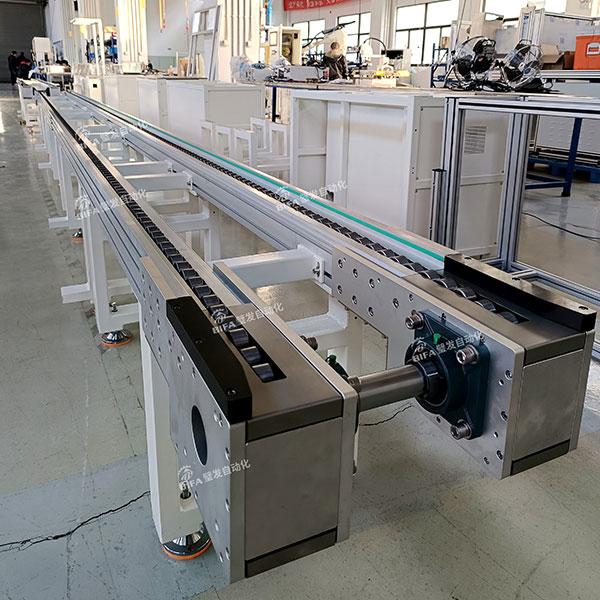
Automotive conveyor line built by BIFA

Case studies

Conveying lines in production, and what they had to solve

Six projects, in the words an engineer would use: the constraint, the modules that answered it, and the numbers the line runs at today.

Battery module assembly pallet loop

Battery module assembly

A 96 m pallet loop with 14 lift-locate stations

RFID traceability at carrier level and a vertical-lift return over the aisle — see how it was engineered.

Packaging line conveyors in production

Logistics & peak flow

Peak-season sortation without recirculation

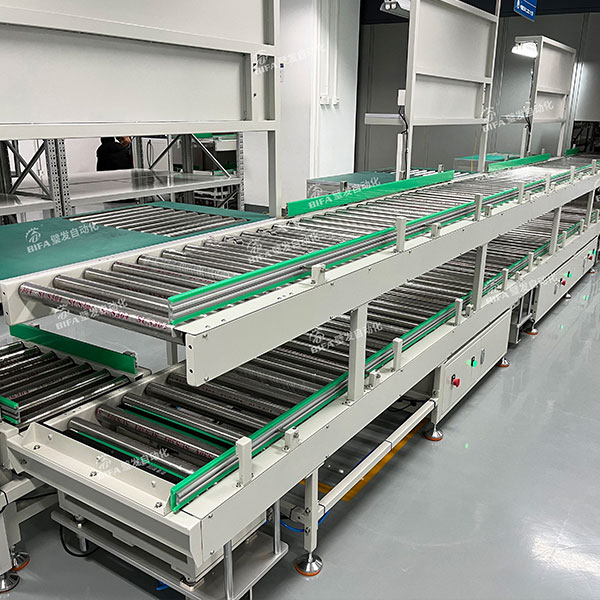
Mechanical accumulation zones sized for peak flow keep cartons moving when the sorter is full.

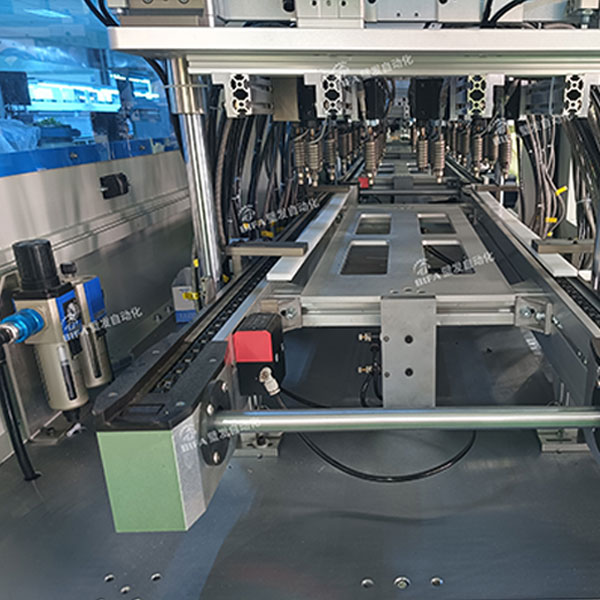
Battery module assembly line — 96 m pallet loop

New energy / Battery

Battery module assembly line — 96 m pallet loop

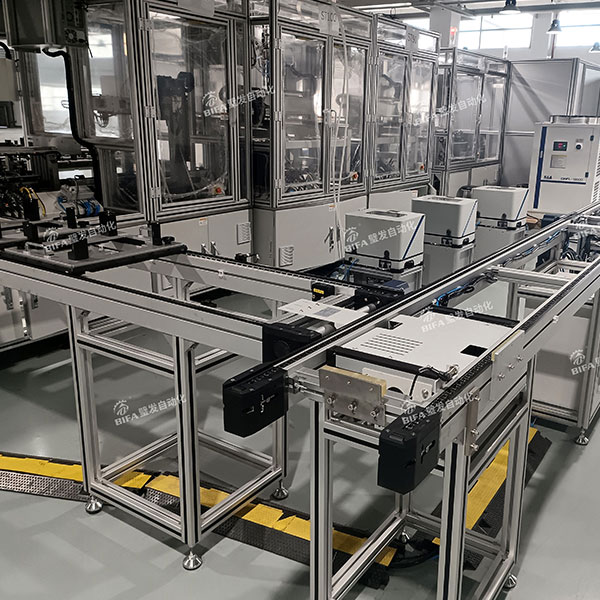
Double-speed chain pallet loop with 14 lift-locate stations, RFID gates and a mezzanine return using a vertical lift.

  • 96 m loop
  • ±0.1 mm locating
  • 8-week build

Challenge

A tier-1 battery plant needed module and pack assembly on one line, with screwdriving torque data traced to every carrier and no floor space left for buffers between stations.

What BIFA supplied

A BFP double-speed chain loop with accumulating zones replaced the buffers: 14 lift-locate stations pin each pallet to ±0.1 mm, RFID gates write the torque data to the MES, and a BFV vertical lift returns empty carriers over the aisle.

Result

  • Footprint cut by 18 % — accumulation replaced physical buffers
  • Traceability down to carrier level, accepted at first audit
  • Commissioned in 3 weeks on site after an 8-hour FAT

Modules in this line
3C electronics test & packing line

3C & Electronics

3C electronics test & packing line

ESD belt conveyor network with mini-belt test benches, barcode gates and lift-transfer divert to rework.

  • ESD-safe
  • 22 stations
  • 12 m/min

Challenge

The customer moved from manual test benches to an in-line flow and could not accept a single ESD defect, nor a line stop to change product mix.

What BIFA supplied

Antistatic PVC belts on anodized frames with conductive wear strips, mini belt test benches fed by lift-transfer units, and barcode gates that route boards to rework without touching the main flow.

Result

  • Surface resistance held inside the ESD window at every station
  • Product changeover without stopping the line
  • Rework loop separated from the main flow

Modules in this line

E-commerce sortation infeed — 260 m

Logistics & distribution

E-commerce sortation infeed — 260 m

Roller conveyor network with powered 90° curves, multi-wedge zones and accumulation feeding a cross-belt sorter.

  • 260 m network
  • 4,200 pcs/h
  • 6 curves

Challenge

An integrator needed a sortation infeed that could absorb peaks from six packing stations without recirculating cartons back to the sorters.

What BIFA supplied

Powered 90° multi-wedge roller modules with mechanical accumulation zones, merge nodes sized for peak flow, and two BFV vertical lifts linking the mezzanine to the sorter deck.

Result

  • 4,200 pcs/h sustained infeed at peak
  • Zero-pressure accumulation stops carton damage
  • Modules shipped in three lots matched to site milestones

Modules in this line

Appliance final assembly & test

Home appliance

Appliance final assembly & test

Pallet conveyor with indexing stops, robot screwdriving cells and reject gates served by lift-transfer units.

  • 36 pallets
  • 2 robots
  • 99.2% OEE

Challenge

Two robots and twelve manual stations had to work on the same flow, with the appliance held hard enough for screwdriving and vision inspection.

What BIFA supplied

A BFP pallet loop with indexing stops at the manual stations and lift-locate units under the robot and vision cells; reject gates are served by BFTU units so a failed unit leaves the loop without stopping production.

Result

  • 99.2 % OEE measured over the first six months
  • One pallet design carries four appliance sizes
  • A single spare-parts kit covers all 36 pallets and drives

Modules in this line

Beverage filling hall — flexible top chain

Food & beverage

Beverage filling hall — flexible top chain

Washdown stainless flexible chain layout linking filler, labeller, shrink-wrappers and palletiser in a single drive run.

  • SUS304 wet area
  • 5 machines linked
  • 1 drive per run

Challenge

Five machines from four suppliers had to be linked in a hall with daily washdown and almost no free floor space.

What BIFA supplied

A BFRXL flexible chain layout with 175 mm and 263 mm chains, 90° and 180° disc curves, hygienic wear strips and sloped drainage — one drive carries the whole run, curves included.

Result

  • Layout closed in a hall 40 % narrower than the original plan
  • Washdown-ready, no water traps at transfer points
  • Changeover to a new bottle format without new modules

Modules in this line

Pharma cartoning infeed — 8 timing belt lanes

Personal care & pharma

Pharma cartoning infeed — 8 timing belt lanes

Eight independently driven timing belt lanes feeding a cartoner, each speed-matched to the machine.

  • 8 lanes
  • ±0.2 mm spacing
  • Gentle handling

Challenge

Small cartons had to be spaced to the cartoner pocket pitch with no slip, while the operator loads the lanes by hand and must be able to stop any single lane.

What BIFA supplied

Positive-drive PU steel-cord timing belts — tooth engagement instead of friction — on eight separately driven lanes with hand-load infeed, low-level sensors and lane-level stop buttons.

Result

  • Spacing held at ±0.2 mm at production speed
  • Rejects from lane misalignment eliminated
  • Operator can stop and reload one lane while the rest run

Modules in this line

Tell us your load case

Attach a drawing or a short spec — our engineers reply within 72 hours with a layout proposal and budgetary price.

  • 72 h engineering response
  • GA drawing & BOM before production
  • CE · ISO 9001 · COO

Or email us directly at info2@bifaconveyor.com